Product and Service Supply Portfolio
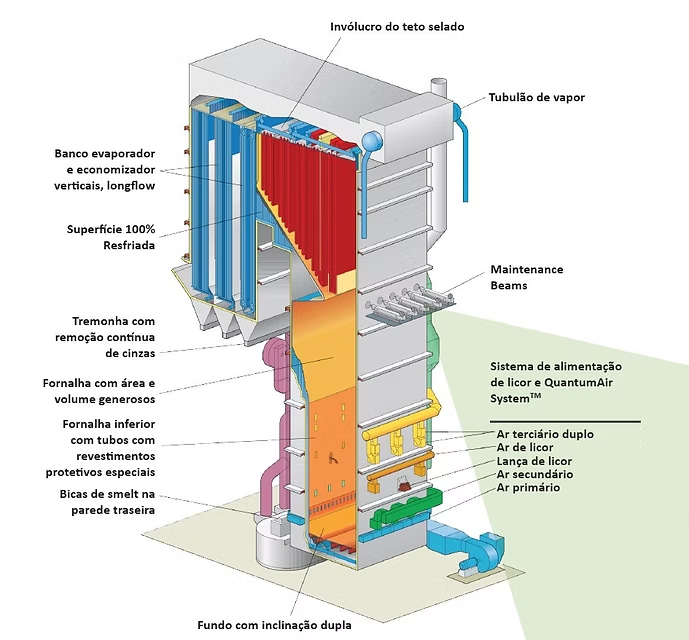
Developed for the Pulp and Paper industry, HPB/B&W Chemical Recovery Boilers provide high availability, safe operation, and reduced maintenance.
The concentrated black liquor, a by-product from the pulp and paper production process, is introduced into the furnace along with the combustion air.
Its combustion results in sodium compounds which, after treatment, are reconverted into white liquor, one of the raw materials used in pulp and paper production.
In addition, the heat released during combustion is recovered by the boiler, generating steam that can be used for process needs or for power generation.
Characteristics
Combustível auxiliar: Gás natural e/ou óleo
Combustível: Licor negro
Temperatura do Vapor: Até 515 °C
Pressão do Vapor: Até 128,5 kgf/cm²
Capacidade: Até 4.500 t/dia de sólidos secos